
With the resurgence of the electronics interconnect manufacturing industry, there is renewed emphasis on automated optical inspection (AOI).
Long-time users are in the market for new and improved technology, while other companies are ready to implement AOI on a wider scale.
AOI suppliers, of whom there are more than 30, are clamouring for attention and a way to differentiate themselves in a crowded market. Price competition has thinned profit margins for both users and vendors, and yet AOI has still not achieved its original performance goals.
Today, inline systems are available for as little as 70 000 Euros in Europe – where volumes are low and support requirements are high. Prices dip as low as $50 000 in China – the mother of all price markets. Many vendors have recently begun to offer bench-top models in addition to inline offerings in the hopes of capturing more market share.
On the user side, companies have begun re-evaluating their AOI strategies. Millions of dollars have been spent in some cases; yet in most factories, an operator is standing at every machine to verify defects. The issue of false alarms has become one of the keys to unlocking the potential of AOI. One primary goal has been that AOI is used most effectively as a feedback tool for yield improvement.
The reality is that many users are simply ‘inspecting defects out’ of the product, and the data from an AOI system is so corrupted by false alarms and questionable defect categorisation that the information generated may be functionally useless for statistical process control (SPC).
A recent evaluation at a large European-based automotive electronics manufacturing services (EMS) company illustrates this. This company has more than 20 conveyorised AOI systems installed, but instead of operating them in line, has opted to create staffed work cells to perform inspection.
It was found that, because of high defect call rates, direct operator involvement was necessary after every inspection cycle; thus, the inline AOI process had become a bottleneck and reduced overall line productivity. The labour savings and improved yields that were expected had not occurred. While end-of-line defects had been reduced, there was no significant reduction in rework – indicating that the pre- and post-reflow inspection data generated was not leading to process optimisation.
This same EMS firm then decided that, because it was not using the conveyorised systems as they were intended, it would also evaluate bench-top systems. It is important to note that this is a plant producing more than 10 000 assemblies a day and is well-versed in six sigma manufacturing practices. We may see this trend spread.
Solder inspection revisited
Another trend has been a reassessment of solder inspection in line. Reviewing the AOI evaluation specifications of five years ago, the solder inspection criteria included excess and insufficient solder, bridging, microvoids, ‘excess’ voiding, shorts, opens, cracks, etc.
All of these parameters are critical, but programming for full solder inspection can, in some cases, take a week. Even then, false alarm rates are often high. In some cases, AOI systems have captured three to four defects on a panel with hundreds of false alarms. In verification, operator acuity is impaired when verifying panels with high numbers of false calls – as real defects inevitably escape.
In a high-mix/low-volume (HMLV) environment, time is of the essence; when parts must ship quickly, programming time is a paramount issue. Additional and angled cameras also impact programming time, inspection time and false alarm rates. Today, many users are attempting to find a balance between defect captures and low false alarms while keeping the line running. When dealing with the inherently unstable and non-repeatable images of solder fillets, the user must strike a fine balance. The operating guideline is ‘Keep it simple.’
Time to first board
With the predominance of HMLV manufacturing in North America and Europe, the semantics of programming and debugging time has become another issue. Interpretations abound, but the crux is that when evaluating AOI systems, you must look at the time it takes between the moment the programmer begins and the time the operator pushes the button on the first inspection cycle.
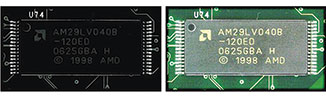
In some cases, programming is quoted in minutes, while debugging is not discussed. In others, the programming process can be daunting, but debug is simple. In the end, the user must assess the overall time it takes to run the first panel effectively. (See Figure 1)
Proper use of AOI is still an issue, even in large manufacturing installations with years of experience. When visiting a large EMS manufacturer recently, it was found that the operators set the AOI parameters wider to reduce the number of alarms, rather than adjusting the production process to reflect the data developed from AOI. This defeats the original purpose of AOI.
Proper and regular training is critical for successful implementation, and cannot be overemphasised. An AOI system that may cost several hundreds of thousands of dollars is only as good as the training of the operator running it. Between turnover and human nature, the system is only as good as its weakest link. Well-trained operators produce better results.
At many companies, price is the driving factor. With AOI, this can be a fatal mistake. A false sense of security can be engendered and real defects escape, with significant consequences. Up to 25% of all AOI systems sold to date are languishing unused. Unmet expectations abound, and we are seeing second-generation implementation of the technology at many companies.
The long-term goal must be process improvement. It takes good equipment, well-trained operators, and accurate data to realise the expectations of AOI.
Where Marantz comes in
AOI systems offered by Marantz have been expressly designed to address many of the issues identified above. The very existence of the Marantz AOI product range came from dissatisfaction with commercially available equipment back in the mid-1990s when Marantz engineers failed to find a system that would meet their needs in manufacturing the company’s acclaimed audio products. So they designed their own.
A few turns of the evolutionary cycle later, and the company has a product range that includes powerful benchtop systems – acknowledging that effective AOI usage demands an operator. But key across the board to the Marantz solutions is 24-bit colour imaging.
Most vendors deploy only 8-bit greyscale. 24-bit colour demands a powerful graphics processing engine but goes a long way to minimising false alarms by improving image clarity and helping to separate components and solder images from the background board or substrate (see Figure 1.) It also enables the Marantz equipment to identify colour as part of the inspection process – for example with colour coded components.
Innovative angled illumination, along with coloured lighting, further adds to the detecting capabilities, particularly with solder fillets. Even though reflowed solder pads are silver-grey, it’s surprising how the selective and calculated use of coloured illumination and 24-bit processing reveals significantly more than a grey-scale engine.
So how do Marantz AOI systems cope with the burden of 24-bit image processing? They all use powerful Apple Mac computers – just like almost every other professional in the graphics industry. And no, operators don’t get iTunes loaded as standard!
For more information contact Zetech, +27 11 609 1244, orliain@icon.co.za, www.zetech.co.za
| Tel: | +27 11 609 1244 |
| Email: | zetech@zetech.co.za |
| www: | www.zetech.co.za |
| Articles: | More information and articles about ZETECH ONE |




© Technews Publishing (Pty) Ltd | All Rights Reserved
 printer friendly version